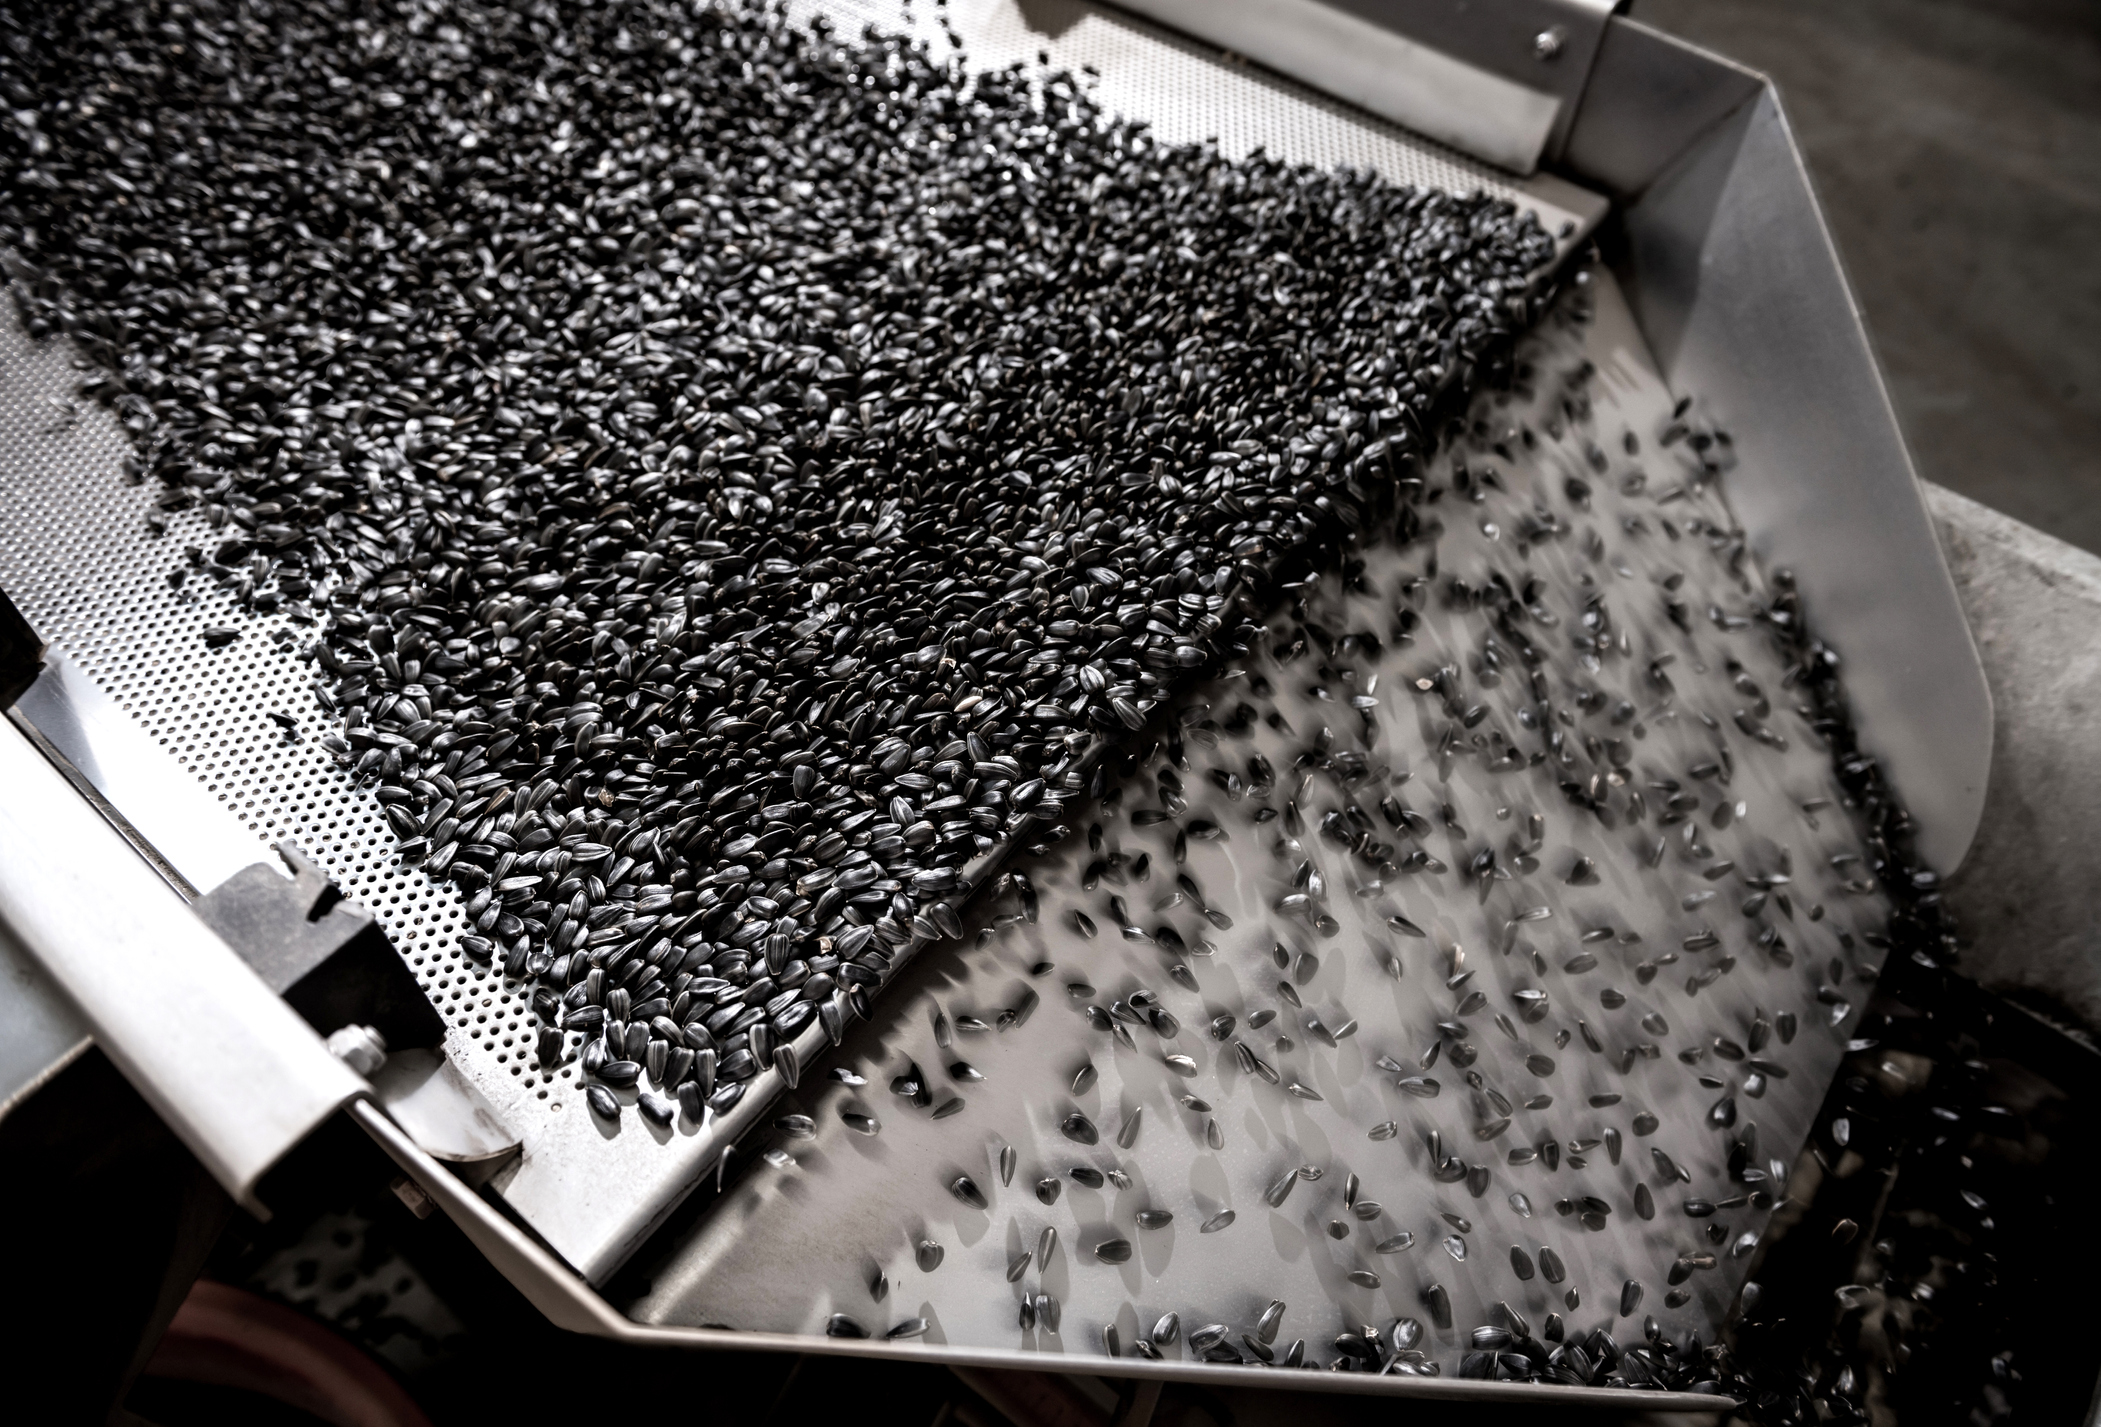
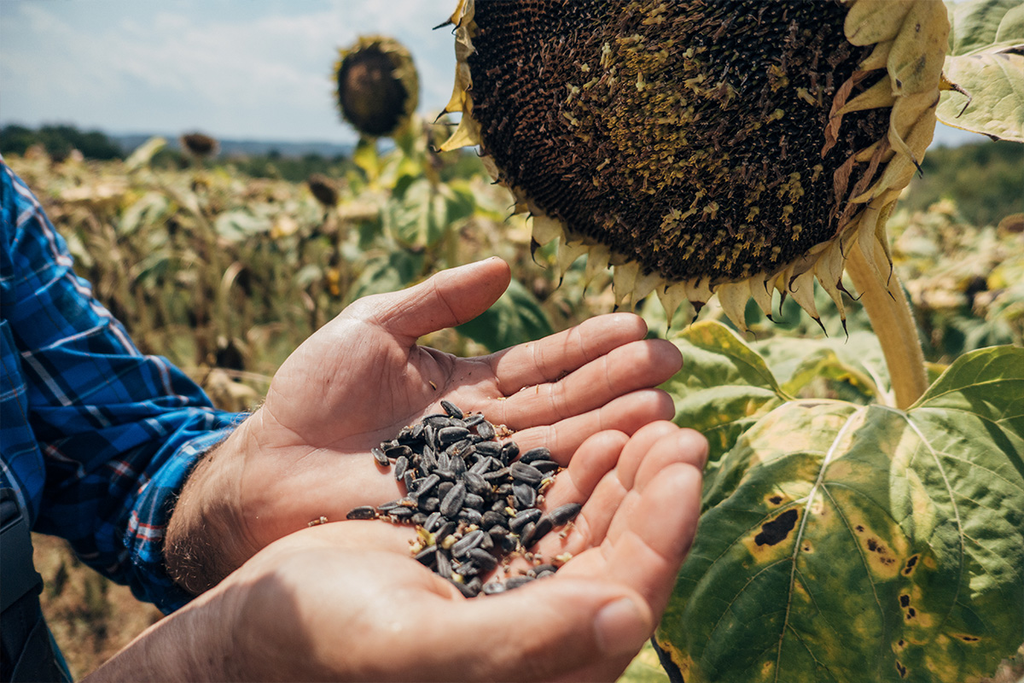
After more than three decades of processing sunflower seeds with an Anderson Hivex™ Expander, a solvent extraction plant in Greece was ready for its next phase of growth. When rising demand for sunflower oil and meal called for an increase in capacity, the oil mill turned to Anderson to guide the commissioning process for another piece of oilseed processing equipment.
The processor installed a second machine, a 10-inch Anderson Hivex™ Expander sized to process 350 tons per day, with the goal of bringing its plant’s combined capacity to 700 tons per day. Anderson’s engineers recently traveled to Greece to commission the new Expander and assist the plant’s operators with equipment startup and calibration.
Within just a few days, Anderson’s extraction experts helped the operators stabilize the machine to start producing quality sunflower collets at 75% capacity. Here’s how Anderson’s commissioning process positioned the plant for a controlled ramp-up to full production.
The challenge of increasing capacity with a tough seed
Established in the late 70s and running Anderson equipment since the 90s, this Greek oil mill mainly processes sunflower seed—which can be a challenging material for a couple of reasons:
- First, the thick hull or shell that covers the seed poses a significant challenge, especially since this processor handles whole sunflower seed without dehulling. These abrasive hulls can exacerbate wear-and-tear on processing equipment.
- Second, sunflower seeds can contain more than twice as much oil by weight as soybeans, which most extraction systems are designed to process. The excess oil can clog standard processing equipment, requiring an additional pre-pressing step before seeds head to the extractor.
To prepare high-oil seeds for extraction, processors typically pre-press material to remove some oil so it behaves more like soybean in the extractor. However, these pre-press cakes aren’t very conducive to solvent extraction. Their irregular shape and compressed structure leave pockets of empty space where solvent can channel around the material instead of permeating it to dissolve the oil, which can increase solvent holdup, reduce oil recovery, and restrict extractor capacity.
Ultimately, the processor needed to expand capacity without disrupting its established solvent extraction process. This required durable equipment that could handle tough hulls while effectively preparing the high-fat material for more efficient extraction.
The solution: Commissioning the Hivex™ Expander
To address these challenges, the processor installed a 10-inch Anderson Hivex™ Expander sized to handle 350 tons of sunflower seed per day, optimizing the solvent extraction process by transforming sunflower seeds to maximize oil recovery.
Using steam-generated heat, a rotating screw propels pre-pressed product through the Expander—generating a high-pressure, high-temperature, high-shear environment that quickly cooks and compresses the seed material while rupturing the oil-bearing cells. The free oil drains into a drainage cage, preventing the excess oil from flooding the machine or downstream conveyors. When the hot, compressed material exits the Expander under extreme pressure, the sudden atmospheric drop causes the moisture to instantly vaporize, creating a network of pores that allow solvent to permeate the material more evenly during extraction.
Anderson’s patented Expander offers several key benefits for the processor, including:
- Increased capacity, allowing the extractor to accept 20-25% more oilseed by compressing the seed material.
- Reduced solvent exposure, enabling solvent to drain through the porous collects more effectively.
- Reduced solvent recovery, making it easier to remove the residual solvent held up in the products.
- Maximum oil recovery, improving the efficiency of the downstream extraction process.
But achieving these benefits requires a careful commissioning process to calibrate the Expander for optimal operation. During startup, Anderson’s engineers gradually increased the screw feeder speed while adjusting pressure on the choke—monitoring these conditions closely while evaluating oil drainage through the cage and collet quality at the discharge.
The results: A controlled path to full capacity
The Greek facility’s new Expander began processing sunflower seed less than 10 minutes after initial startup. Within a few hours, Anderson’s engineers worked alongside the plant’s experienced operators to stabilize the operating temperature and fine-tune the feed rate and choke pressure to produce consistent collets with visible oil drainage.
By the time it reached about 75% capacity, the Expander was producing good quality collets with residual oil levels around 22-24%, representing ideal conditions for optimal solvent extraction. After the commissioning process, which only lasted a few days, the processor was ready to gradually ramp up the machine to full capacity while achieving the expected product quality.
Once fully ramped up, the new Hivex™ Expander will work alongside the plant’s original Anderson equipment to reach the combined processing target of 700 tons per day. But Anderson’s support doesn’t end there. Having commissioned more than 12,000 pieces of equipment for over 1,000 plant installations in 100 countries, and processed more than 80 different oilseed varieties, Anderson’s extraction experts know how to troubleshoot processing issues and keep plants running at peak production capacity.
After all, a successful commissioning process isn’t just about installing a new machine but also about supporting downstream extraction efficiency, production capacity, and product quality to ensure a long-term return on investment for processors.
Contact Anderson International to schedule your new equipment installation, plant startup, and commissioning process with confidence.